
|
Quantity
|
Total
|
||
|
|
|||
|
|
|||
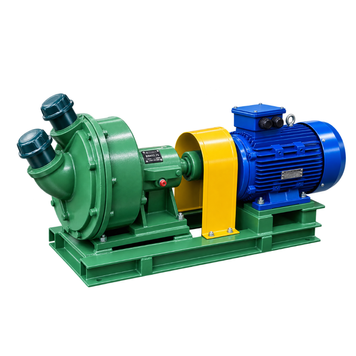
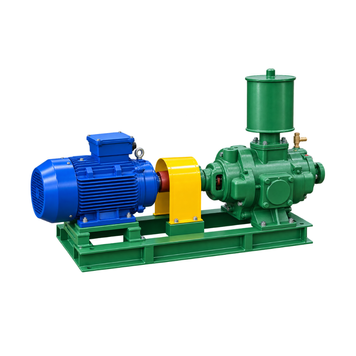
Liquid ring vacuum pumps are industrial units designed to generate and maintain vacuum by evacuating air, gases and gas-vapor mixtures from closed process systems. This pump technology is particularly suitable for applications involving humid gases, vapors and processes where some liquid carryover may occur.
The operating principle is based on an eccentrically positioned impeller rotating inside the pump casing. Centrifugal force causes the operating liquid, typically water, to form a rotating liquid ring. The changing volume between the impeller blades and the liquid ring provides continuous gas suction, compression and discharge. The operating liquid also provides sealing and absorbs heat generated during compression.
Liquid ring vacuum technology is suitable for demanding industrial processes involving moisture and high vapor loads. These pumps are widely used in chemical and petrochemical processing, power generation, pulp and paper production, food processing, mining, filtration, drying, evaporation and other industrial applications.
This category includes VVN liquid ring vacuum pumps with different capacities and operating parameters. When selecting a pump, it is important to consider the required pumping capacity, operating pressure, characteristics and temperature of the pumped gas, operating liquid consumption, electric motor power and the specific requirements of the industrial vacuum system.